Working pressure, test pressure, and burst pressure describe different parts of an LPG cylinder’s pressure design and verification. They are not interchangeable ratings, and a higher number in one field does not by itself prove that a cylinder is suitable for a market or application. Procurement teams should connect every pressure value to the exact cylinder model, applicable design standard, test method, acceptance criteria, and supporting document before approving an order.
The three values answer different questions. Working pressure addresses the rated in-service pressure basis. Test pressure is the controlled pressure applied during a specified non-destructive verification. Burst pressure is determined in a destructive test used to evaluate ultimate structural behavior or design qualification. Mixing them can create false comparisons between suppliers or lead buyers to request a test that is not appropriate for routine production acceptance.
Terminology also varies by code and market. Service pressure, working pressure, design pressure, proof pressure, test pressure, and minimum burst pressure may have related but non-identical meanings. The governing document and cylinder marking should control the interpretation, not a generic ratio found in a catalog or online discussion.
Working pressure is the pressure rating associated with intended service under the specified design framework. It should not be confused with the changing vapor pressure of the LPG contents, which depends strongly on composition and temperature. The purchasing specification needs to identify which term the applicable code uses, where the rating appears, and whether the valve and other pressure-retaining components use compatible ratings.
A buyer should not select a cylinder merely because its working pressure is greater than a pressure observed in another market. Suitability also depends on material, wall design, welded construction, heat treatment where applicable, valve system, fill limits, environmental conditions, and the complete conformity route. Pressure is one controlled field within a larger approved design.
Test pressure is applied under a defined procedure to check required structural or leak-tightness performance without intentionally rupturing the cylinder. The medium, pressure level, hold time, measurement method, equipment calibration, permitted expansion, leakage criteria, and test frequency should come from the applicable standard and approved manufacturing plan.
Hydrostatic testing uses a liquid test medium and can support measurements or checks required by the procedure. A pneumatic leak test, when specified, serves a different purpose and presents different hazards. Procurement documents should never use the broad phrase pressure tested as sufficient evidence. They should state the exact test, stage of production, acceptance criteria, and record required.
Burst pressure is the pressure at which the test specimen ultimately fails during a controlled destructive test. A standard may instead specify a minimum required burst pressure, a ratio, a failure mode, or behavior before rupture. These are design or qualification controls, not operating targets. A cylinder that undergoes a burst test is not returned to service or shipped as saleable product.
Buyers should ask which sample, batch, design family, and revision the burst result represents. The report should identify the cylinder, test setup, pressure-time record, observed failure location and mode, and acceptance basis. A single headline number without traceability cannot demonstrate that the offered production configuration matches the tested design.
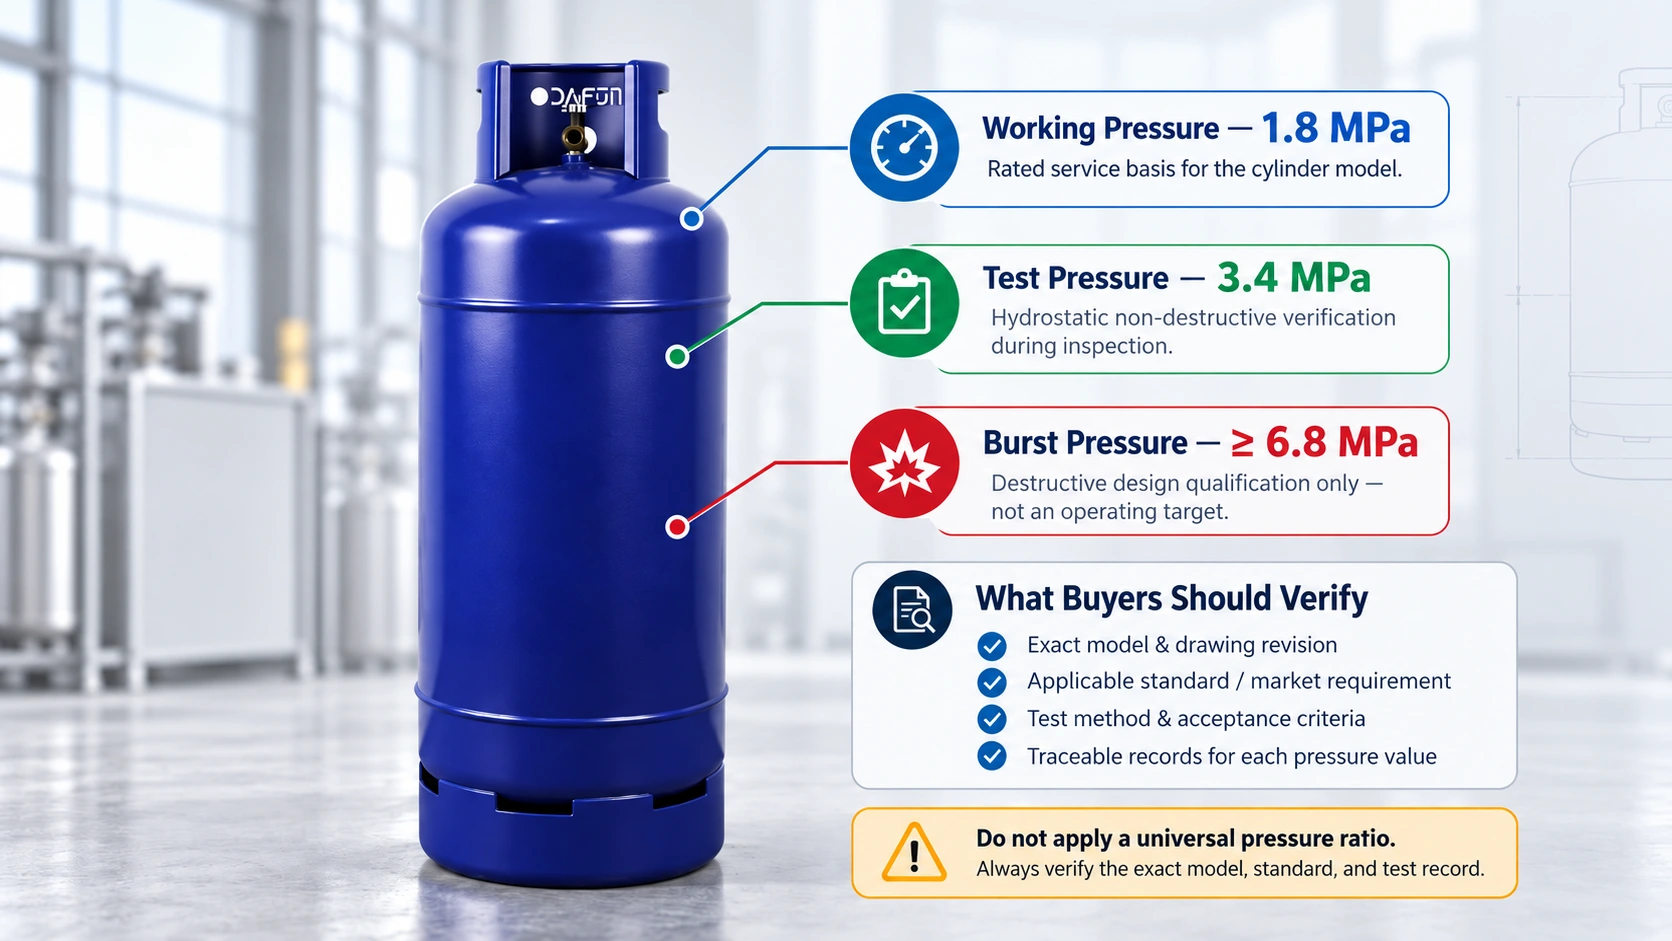
Ratios between working, test, and minimum burst pressures are often used within particular standards, but there is no safe universal multiplier for every LPG cylinder. Requirements can change with jurisdiction, cylinder construction, capacity, material, design route, and standard edition. Even when two quotations show the same ratio, their test methods and acceptance rules may differ.
For that reason, the RFQ should request the applicable clause or approved specification for each pressure value. Procurement teams should compare like with like: the same terminology, unit, reference temperature or condition where relevant, design standard, and test purpose. Unit conversion between MPa, bar, and psi should be checked independently, but conversion does not resolve a difference in definitions.
A three-value table is useful only when each number is tied to evidence. Add the following fields to the technical bid comparison and leave a field open when the supplier has not provided a controlled source.
| Pressure term | Value and unit | Required evidence | Procurement decision |
|---|---|---|---|
| Working or service | Exact rated value | Marking, drawing, standard and model | Matches destination and full assembly |
| Test or proof | Exact value and method | Procedure, calibrated equipment and acceptance record | Correct test applied at required stage |
| Minimum burst | Requirement and actual result if available | Qualification report, sample identity and failure record | Traceable to offered design revision |
这 Mintai Cylinder 45 kg LPG cylinder page provides a product-specific example: it lists working pressure of 1.8 MPa and test pressure of 3.4 MPa for that page’s configuration. Those figures should not be generalized to another size, material, valve arrangement, destination, or design standard. Buyers can review other available configurations in the company’s LPG cylinder product range and request documentation for the exact offered model.
First, normalize the terminology and units without changing the supplier’s underlying definition. Second, verify that each figure belongs to the quoted cylinder and current drawing revision. Third, separate routine production checks from design qualification tests. Finally, close every difference with a written technical clarification rather than selecting the highest pressure figure.
Pressure ratings should also be reviewed with valve selection and filling compatibility. A cylinder shell rating does not establish that the valve, relief arrangement, regulator connection, and authorized filling process are suitable. Mintai Cylinder’s valve compatibility guide can support that adjacent review, while the pressure documentation remains model- and standard-specific.
Working pressure, test pressure, and burst pressure form a connected evidence chain, but they serve different purposes. A defensible purchase specification identifies the governing standard, exact model, definition, value, unit, test method, sampling level, acceptance criteria, and traceable record for each field. Avoid universal ratios and unsupported comparisons. To request a technical review from 民泰圆柱体, provide the destination market, applicable standard, cylinder capacity, material, valve configuration, required pressure terms, drawing, quantity, and inspection expectations.
No. Test pressure is applied under a specified verification procedure. The working or service rating used for operation must be identified separately under the applicable cylinder standard.
No. The result is meaningful only with the design requirement, specimen identity, test method, failure behavior, and traceability to the offered production configuration.
Only when the governing standard or approved specification provides the applicable relationship. A generic multiplier should not replace the required clause and test method.
No. A hydrostatic proof or expansion test is normally non-destructive when passed. A burst test intentionally continues to ultimate failure on a designated specimen.
Include the applicable standard, exact pressure terms and units, test method, acceptance criteria, sampling level, required reports, model and drawing revision, valve configuration, destination, and inspection plan.