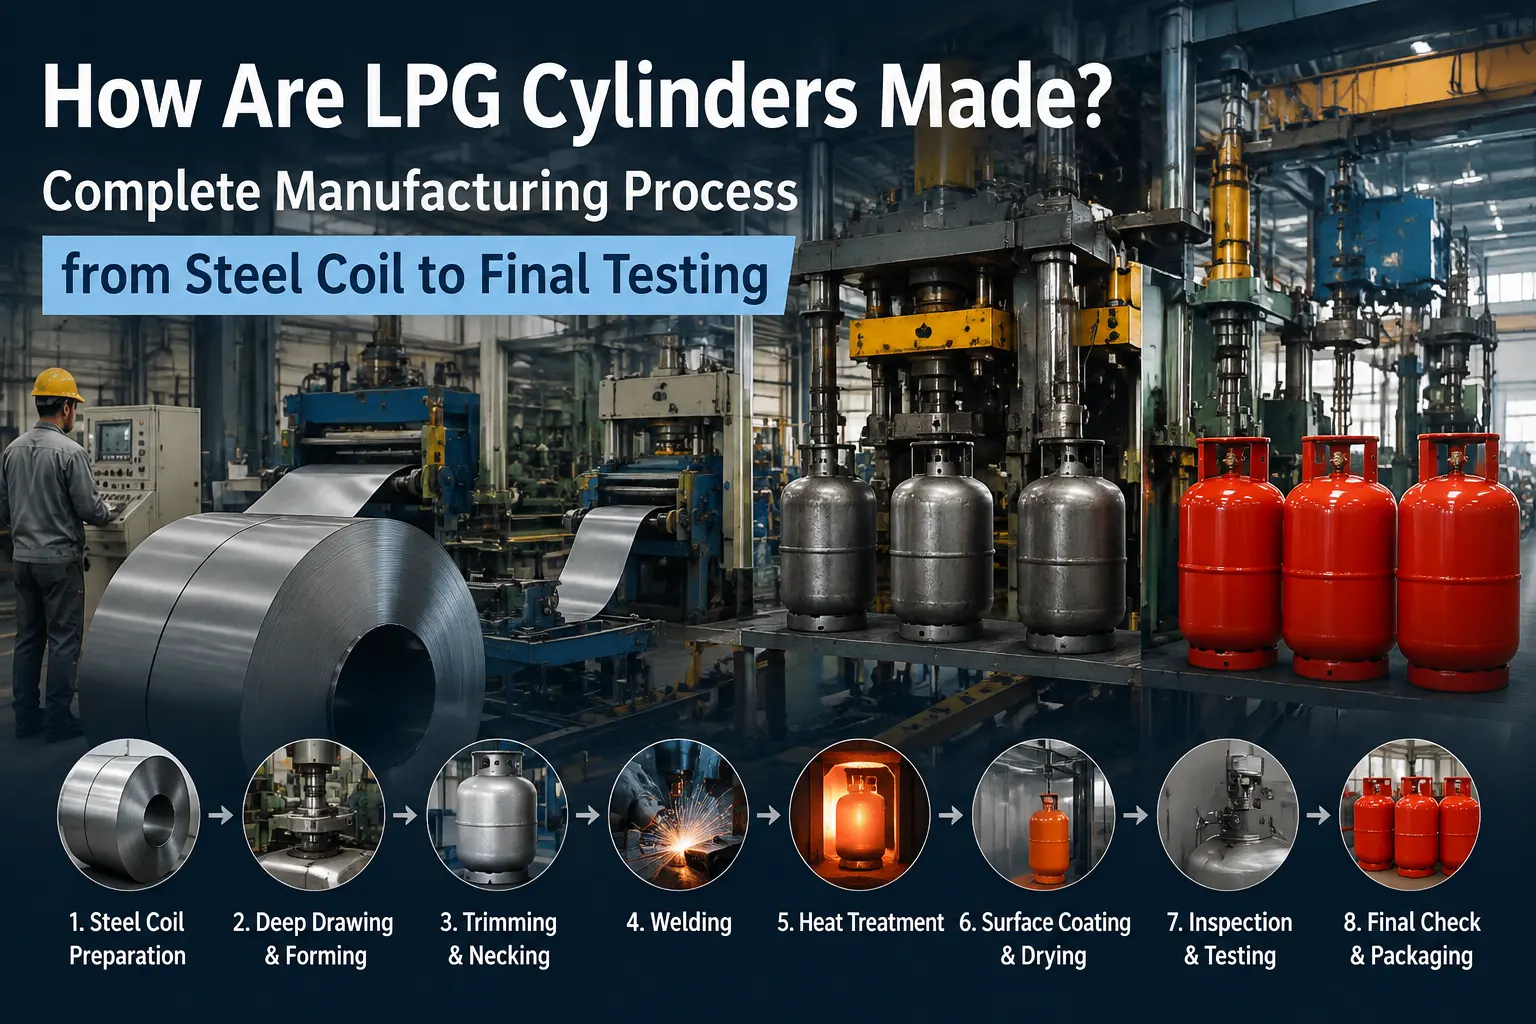
For B2B buyers, understanding the LPG cylinder manufacturing process is a practical way to judge whether a supplier can control shell geometry, weld integrity, pressure resistance, surface protection, and final tightness. A welded steel LPG cylinder typically moves from steel preparation to blanking, deep drawing, shell finishing, component assembly, circumferential welding, heat treatment, surface preparation, coating, and testing. The exact sequence and inspection plan depend on the cylinder design, applicable standard, target market, and approved manufacturing procedure.
Mintai’s published LPG cylinder production process includes blanking and cutting discs, deep drawing, trimming and joggling, circumferential welding, heat treatment, shot blasting, powder painting, and air leakage testing.
ISO 22991, which covers transportable refillable welded steel LPG cylinders, addresses material, design, construction, workmanship, manufacturing procedures, and tests at manufacture. For procurement, this means quality should be judged across the process rather than only by the finished paint surface or one final test.
| Manufacturing stage | Main output | What a B2B buyer should verify |
|---|---|---|
| Material preparation | Production-ready steel | Grade, thickness, identification, traceability |
| Blanking | Circular steel discs | Diameter, edge and surface condition |
| Deep drawing | Upper and lower shells | Shape, dimensions, forming defects |
| Trimming and joggling | Welding-ready shells | Edge preparation and fit-up |
| Component assembly | Positioned fittings | Drawing conformity and location |
| Circumferential welding | Closed cylinder body | Weld consistency and inspection |
| Heat treatment | Processed pressure body | Controlled process and records |
| Surface preparation | Clean steel surface | Coating readiness |
| Coating and finishing | Finished exterior | Coverage, marking, finish |
| Testing and inspection | Accepted cylinder | Pressure, tightness and test records |
The body of a welded steel LPG cylinder starts as flat steel. Depending on the production route, steel coil or sheet is prepared and cut into circular blanks sized for the required shell geometry.
A circular blank needs more than the correct nominal diameter. Steel grade and thickness must match the approved cylinder specification, and the blank should have suitable surface and edge condition for forming. Damaged edges, inconsistent thickness, incorrect dimensions, or poor material identification can create deep-drawing problems or weaken traceability.
Procurement questions should include: What material is specified? How is incoming steel identified? How are blank dimensions checked? Can material records be linked to the production batch? Buyers sourcing semi-finished steel discs should also confirm diameter, thickness, grade, edge requirements, quantity, and drawing references before ordering.
Deep drawing converts a flat circular blank into a cup-shaped shell. Upper and lower halves are then trimmed and prepared for accurate fit-up before welding. Joggling creates the required edge geometry according to the manufacturing design.
Cracking, wrinkling, uneven edges, or inconsistent shell dimensions can point to issues with material condition, tooling, lubrication, forming parameters, or dimensional control. Buyers auditing a factory should ask how shell dimensions are checked, how forming defects are classified, and how nonconforming parts are segregated.
A finished cylinder may also include a valve boss or neck connection, guard or collar ring, and foot or base ring. Their geometry and position affect assembly and welding.
Component design should follow the cylinder drawing and market requirements rather than a one-size-fits-all assumption. A guard ring may require specific openings or clearances; a base ring must support the cylinder correctly; and the valve connection must match the approved cylinder and valve configuration.
For custom or replacement sourcing, buyers should confirm the drawing, material, thickness, dimensions, hole pattern, interface details, and finish requirements. Poor fit can create alignment problems, inconsistent weld gaps, distortion, or rework. Semi-finished components are therefore best evaluated as parts of a defined cylinder design, not as generic accessories selected only by outside diameter.
Circumferential welding joins the prepared upper and lower shells into a closed pressure body. Fit-up, welding consistency, and downstream inspection all influence whether the assembly can meet its manufacturing tests.
A buyer does not need confidential machine settings to assess process discipline. More useful questions are how shell alignment is controlled, how welds are inspected, how nonconforming welds are handled, and whether the required procedures and controls are maintained. Possible concerns include porosity, lack of fusion or penetration, undercut, misalignment, and distortion. Acceptance limits should be judged against the approved design and applicable standard rather than a generic checklist.
Forming and welding change the condition of the steel and welded assembly. Where the approved manufacturing process requires heat treatment, it is used to bring the cylinder body into the condition specified for subsequent inspection and service.
For buyers, the key issue is control rather than simply the presence of a furnace. The required cycle, monitoring method, loading practice, records, and acceptance criteria depend on the cylinder specification and standard. If exact temperature or holding-time data matter to an order or audit, they should be verified against the approved process. Mintai lists heat treatment as part of its published production sequence.
After body fabrication, the cylinder surface must be prepared before coating. Rust, oxide scale, welding residue, oil, or other contamination can interfere with coating adhesion and exterior durability.
Shot blasting mechanically cleans and prepares the steel surface before painting or powder coating. Abrasive type, surface condition, and process settings vary by equipment, coating system, and specification, so buyers should not judge the process by one universal steel-shot size.
Inadequate cleaning can contribute to premature coating failure, exposed steel, corrosion, or uneven appearance. For humid, coastal, outdoor, or long logistics cycles, finish and corrosion-protection requirements should be defined in the RFQ and checked against the supplier’s coating specification.
Coating requirements should be specified rather than inferred from color alone. Buyers should confirm color, branding, markings, surface preparation, coating specification, inspection method, and any destination-market requirements.
If coating thickness, adhesion testing, salt-spray performance, or a particular finish system is contractually important, those requirements should be agreed before production.
The applicable test sequence and sampling plan depend on the standard, cylinder design, and approved inspection plan.
Mintai’s LPG cylinder testing and inspection information lists hydraulic testing, tightness testing, bursting testing, mechanical testing, X-ray inspection, water-volume testing, and appearance instrumentation. The site states that each Mintai cylinder undergoes hydraulic testing followed by a tightness test.
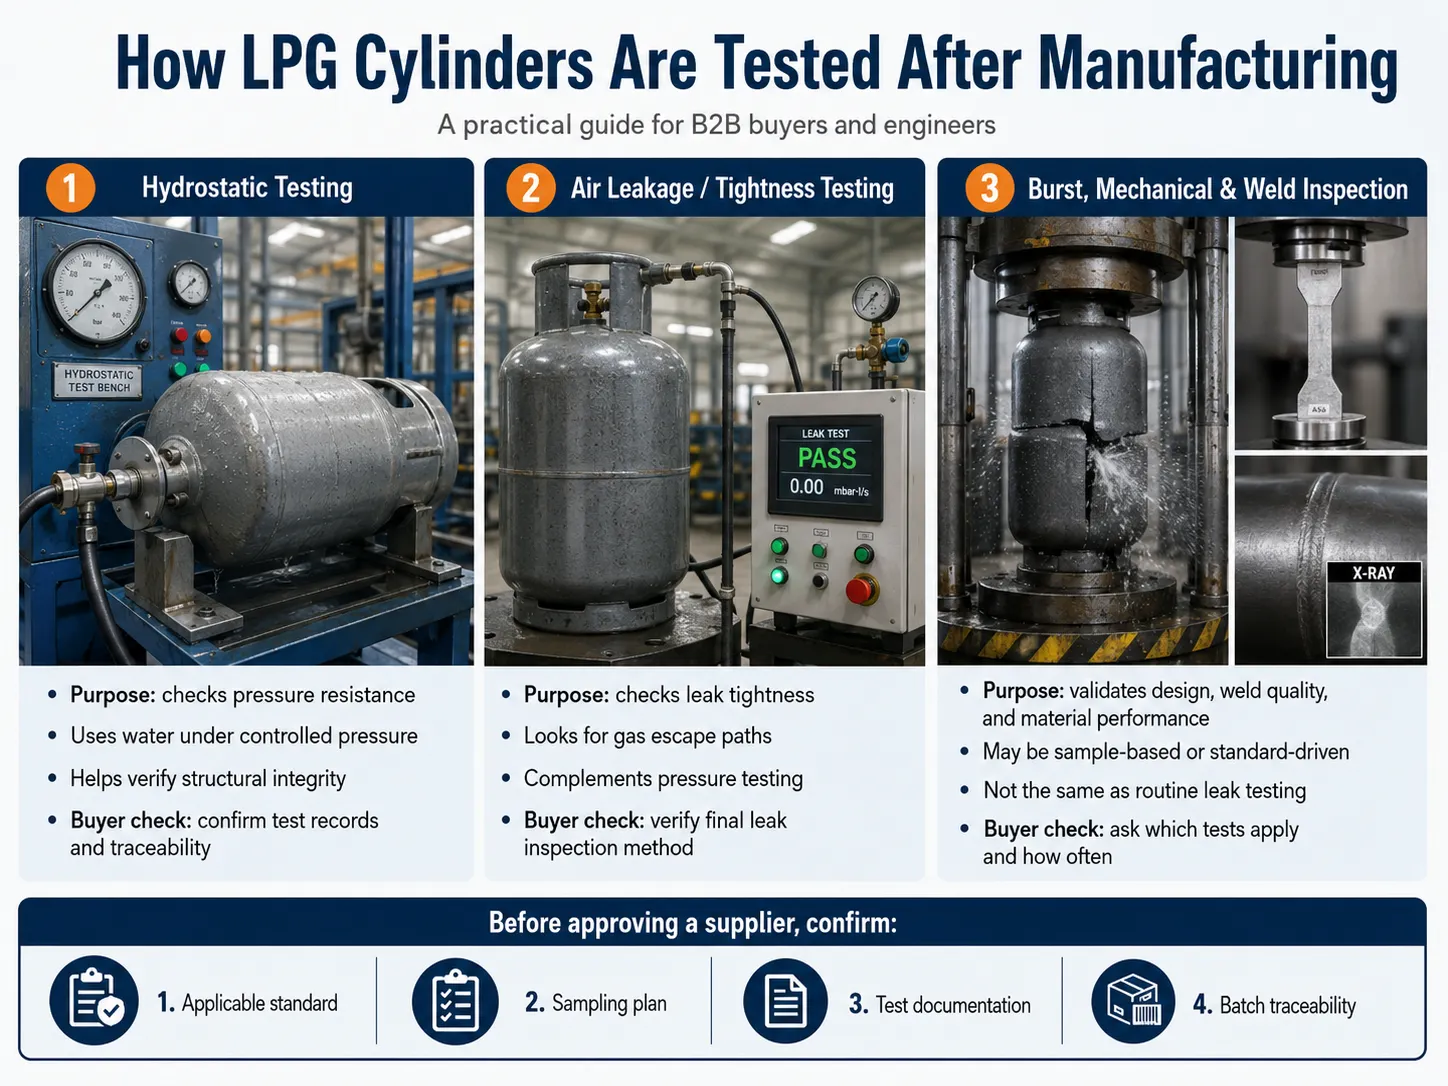
Hydrostatic or hydraulic testing subjects the cylinder to controlled internal water pressure under specified test conditions. Tightness or air-leakage testing addresses a different question: whether gas can escape through leak paths in the completed assembly.
Passing one test should not be treated as proof that every other requirement has been satisfied. Buyers should confirm the required test pressure and procedure against the product specification, ask how results are recorded, and determine how tested cylinders or batches are identified.
Burst testing, mechanical tests, and weld examinations serve purposes different from routine tightness checks. A burst test takes a sample to failure, mechanical testing can evaluate specified material or weld properties, and radiographic examination may be used where required to assess weld quality.
Do not assume that every inspection shown by a supplier is performed on every cylinder. Frequency may be 100 percent, batch-based, sample-based, type-test based, or otherwise defined by the applicable standard and quality plan. Ask which tests apply to the exact model, what the sampling basis is, and which records can be supplied with the order.
A blanking problem can become a forming reject; poor shell fit can complicate welding; inadequate surface preparation can appear as coating failure after shipment.
Cracking, wrinkling, uneven edges, and dimensional variation should trigger review at the forming stage. Weld irregularity, misalignment, or test failures require controlled disposition rather than undocumented cosmetic repair. Heat treatment should follow the approved process, while shot blasting and coating need consistent surface preparation.
The practical prevention method is a linked control plan: verify incoming material, inspect forming before welding, inspect and test the pressure body, prepare the surface consistently, and retain traceable records. Buyers can use the same sequence during supplier audits instead of relying on final appearance alone.
A supplier should be evaluated on evidence that the process is controlled, not only on capacity claims or sample appearance. Useful checkpoints include material traceability, repeatable forming, documented welding control, heat-treatment control where applicable, test capability, nonconformance handling, final inspection, and batch traceability.
Mintai operates as an एलपीजी सिलेंडर निर्माता specializing in LPG cylinders. Its website states that the company has six automated production lines and annual output of about two million cylinders.
A comparable RFQ should identify cylinder capacity and dimensions, destination market, applicable standard or certification requirement, valve/interface requirement, guard and base-ring configuration, coating and color, marking or branding, target quantity, packaging, and inspection-document requirements. If a drawing or approved sample exists, it should be supplied early.
Mintai’s exported product category lists 3 kg, 6 kg, 9 kg, 12.5 kg, 20 kg, and 45 kg/100 lb models. Buyers comparing LPG cylinders for international markets should verify the specification and market requirements of the exact model rather than assume one configuration applies to every destination.
The LPG cylinder manufacturing process is a chain of dependent controls. Steel selection and blanking affect deep drawing; forming accuracy affects weld fit-up; welding and heat treatment affect the pressure body; surface preparation affects coating performance; and the required tests determine whether the cylinder meets its approved criteria.
For B2B procurement, turn the factory flowchart into a verification checklist. Confirm the cylinder specification, material, critical dimensions, manufacturing route, inspection plan, test records, finish, marking, and traceability before placing a bulk order.
For a project with a specific capacity, drawing, destination market, valve configuration, finish, target quantity, or inspection-document package, buyers can request a technical quotation with those details so the requirement can be reviewed against a defined cylinder configuration.
A welded steel LPG cylinder is generally produced through steel preparation, blanking, deep drawing, trimming and fit-up, component assembly, circumferential welding, heat treatment where required, surface preparation, coating, and manufacturing tests. The exact sequence varies with the design, standard, and approved procedure.
Material must match the approved cylinder design and applicable standard. Steel grade, thickness, mechanical properties, and traceability should be verified against the product specification. One grade or thickness should not be assumed to apply to every cylinder size or market.
Deep drawing forms a flat circular steel blank into the curved shell required for a welded cylinder body. Material, tooling, blank size, and forming parameters must be controlled, and shell dimensions and forming quality should be checked before welding.
Testing can include hydraulic or hydrostatic testing, tightness testing, weld examination, burst testing, mechanical testing, dimensional checks, and final visual inspection, depending on the applicable standard and approved inspection plan.
Check material traceability, blanking and forming control, weld inspection, heat-treatment control where applicable, pressure and tightness testing, surface preparation, final inspection, nonconformance handling, and records linking finished cylinders to production batches.